
Acid deliveries and corrosive waste disposal create recurring expenses every time conventional deionization resins need chemical regeneration. Electrodeionization (EDI) uses electricity to continuously regenerate its resins, so EDI purification requires no routine acid or caustic regeneration.
For industrial facilities, that change eliminates regenerant disposal tasks and avoids the scheduled interruptions required by chemical regeneration.
Why Hazardous Chemical Burdens Affect Water Treatment Methods
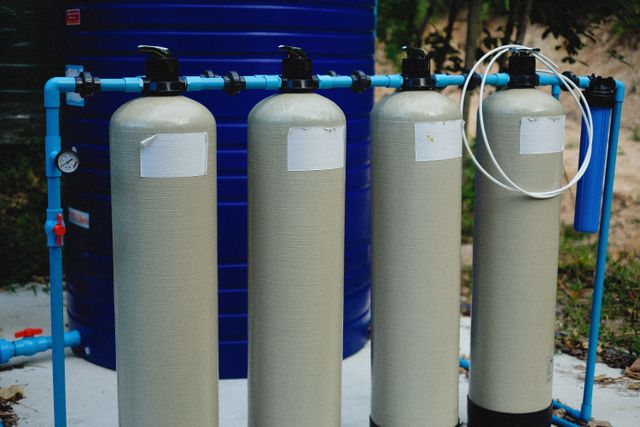
Conventional deionization captures dissolved ions on resin beds, which eventually reach their working capacity. Operators must then regenerate those beds with acid and caustic chemicals before they can resume their purification duty. Facilities must plan around those cycles and monitor outlet purity as the resin approaches exhaustion.
The chemical invoice covers only part of that work. Storage equipment requires maintenance, and operators need time to transfer regenerants and manage spent solutions. Where corrosive discharge requires neutralization, the facility also needs equipment and operating procedures for that step. Each regeneration cycle generates additional waste that calls for appropriate management.
For hazardous waste, disposal costs hinge on classification, as well as the disposal method and transport requirements, according to the Consortia Advancing Standards in Research Administration Information. A quote may include waste characterization and packaging charges, as well as collection fees. Generator status and the distance to an approved disposal facility can also affect the bill.
A useful cost comparison separates regenerant purchases from neutralization equipment and waste-service charges. Engineers can then identify which expenses would stop when electrical regeneration replaces chemical resin restoration. Actual savings will depend on the existing installation and the classification of its waste stream.
How Electrical Regeneration Removes Dissolved Salts
According to MECO, a Grundfos Company, a builder of water purification and pure steam generation systems, EDI purification uses ion-exchange resins to capture dissolved salts and other charged impurities. Electricity continuously restores the resins’ ability to capture these impurities while water flows through the system. Conventional deionization beds need a separate acid or caustic regeneration cycle before they can resume purification.
Before water reaches EDI, reverse osmosis (RO) removes much of the incoming contamination. This sequence allows EDI to focus on the remaining dissolved ions. Engineers select and size both stages based on the incoming water quality and the purity required by the application.
Removing dissolved ions addresses one part of water quality. A laboratory or manufacturing process may also set limits for microorganisms and organic contaminants. Engineers must assess each requirement separately to confirm that the complete system delivers suitable water.
Electrical regeneration requires no routine acid or caustic to restore EDI resins, thereby avoiding the corrosive waste from that step. Other stages may still use chemicals for pretreatment or sanitization. A chemical-use assessment should identify those remaining uses separately from resin regeneration.
How an Integrated RO and EDI System Works
MECO, a Grundfos Company, designed and installed a purified water system for a cardiac and vascular device manufacturer’s expanded quality control laboratory in Temecula, California. The outcome reported up to 50% energy savings through ultra-low-pressure RO membranes and efficient components. The project was completed in five weeks, approximately half the typical lead time.
The company’s packaged systems integrate pretreatment, RO and EDI on a common skid. Integrated controls coordinate operation, and a recirculation mode allows continued operation when the facility draws no product water.
Because the Temecula case study features an integrated installation, its energy figure reflects the combined contribution of RO and EDI. A facility evaluating a similar package would need to compare the proposed RO equipment and electrical resin regeneration against its existing system before estimating savings.
Why Removing Chemical Regeneration Supports Safety and Reliability
The Occupational Safety and Health Administration identifies exposure assessment and specialized containment for corrosive chemicals among its acid or caustic handling considerations. Its guidance also addresses protective equipment and emergency eyewash facilities, which illustrate the practical responsibilities associated with the use of corrosive chemicals.
Removing chemical resin regeneration changes three specific operating tasks:
- Regenerant discharge: The process no longer produces spent acid or caustic regenerant, so it may no longer need dedicated neutralization capacity for that discharge.
- Waste disposal: Operators avoid the collection and disposal activities associated with that regenerant stream.
- Chemical handling: Staff no longer need to receive or transfer acid and caustic compounds solely for resin regeneration.
While traditional purification operations expose staff to corrosive chemicals, protective equipment and emergency facilities remain necessary. Continuous electrical regeneration avoids scheduled interruptions for resin restoration, although maintenance and upstream equipment still affect overall system availability.
How to Evaluate Purity, Operating Costs and Reliability
Engineers comparing water treatment methods should specify the required product quality and confirm the feedwater conditions under which a proposed system can achieve it. For EDI purification, an assessment should distinguish ionic purity from other application requirements, including microbial and organic contaminant control.
Operating-cost comparisons must cover the complete installation. Electricity and maintenance remain part of the budget, while avoided purchases of regenerant and waste-management activities belong on the savings side. Site-specific calculations are a more useful basis for selection than assumptions that all facilities incur the same disposal charges.
During a reliability review, engineers can ask suppliers to explain how controls respond to changes in feedwater pressure or temperature. The service schedule should also identify maintenance tasks and any associated interruptions so that facilities can assess availability across the complete installation.
Frequently Asked Questions About Electrodeionization
Common questions about EDI focus on how it differs from conventional ion exchange and whether it requires chemical regeneration. The answers also clarify how continuous operation supports consistent water quality.
What makes EDI different from traditional ion exchange?
EDI restores its resin capacity electrically during purification. Conventional chemically regenerated ion exchange requires periodic acid or caustic cycles, so operators must coordinate resin restoration with the facility’s water supply needs.
Does EDI eliminate the need for chemical regeneration?
Yes, EDI uses electricity to regenerate its ion exchange resins during operation. Pretreatment or sanitization elsewhere in the system may still require chemicals, so the benefit applies specifically to resin regeneration.
How does EDI improve water quality consistency?
Continuous regeneration helps maintain the resin’s ability to remove ionic impurities during operation. Feedwater conditions and the performance of upstream treatment still influence the product water quality a facility can achieve.
How Smarter Standards Improve Industrial Water Treatment
A shift to electrical resin regeneration removes routine acid or caustic regeneration and the associated corrosive waste stream from industrial water purification.
For future upgrades, engineers can specify the purity required by the application and ask suppliers to document regeneration-related handling tasks, along with the proposed system’s energy and water needs.